Toilet Paper Manufacturing Equipment: A Complete Guide to Production Lines
Selecting the right toilet paper manufacturing equipment is one of the most consequential decisions a tissue converter will make. This guide walks through production line components, workflow mechanics, machine comparisons, procurement strategy, and emerging technology trends — giving B2B procurement managers, engineers, distributors, and OEMs a structured foundation for smarter capital investment. Whether you are scaling an existing operation or entering the modern retail supply chain for the first time, understanding these fundamentals directly affects your output consistency, operational cost, and long-term competitiveness.
Understanding Toilet Paper Manufacturing Equipment: Key Components and Processes
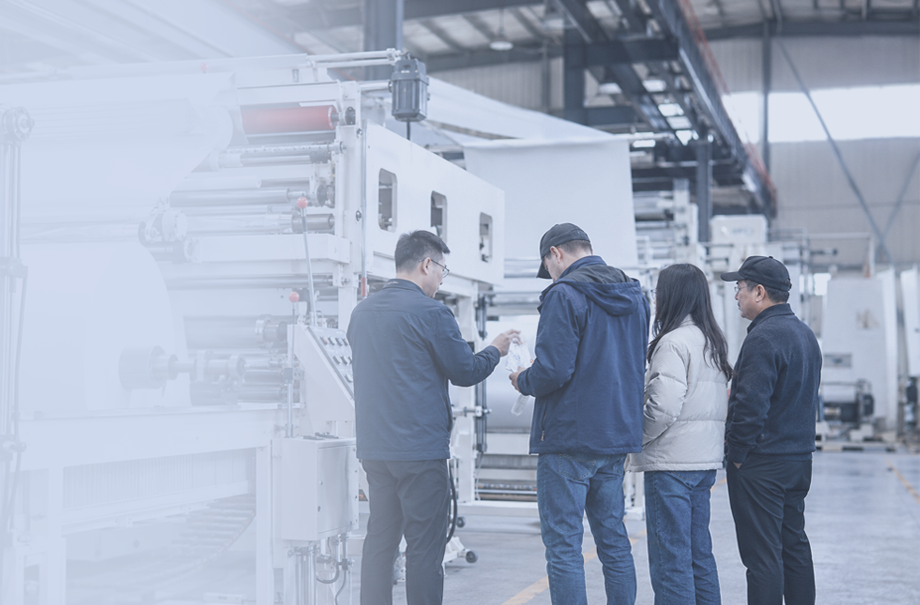
Understanding the toilet paper manufacturing equipment: Key Parts and Steps. A tissue converting line is not just one machine; it's a system with several stages that work together to prepare the next one. Skipping a part or not giving enough information about one makes a bottleneck that slows down production and makes the product less consistent.


Core Machinery Along the Production Line
Most of the time, the converting sequence goes through these stations:
- Jumbo roll unwinding: For unraveling a jumbo roll, a pneumatic filling arm places parent rolls that weigh up to two tons. Every step further down the line depends on the web quality being stable. The HENGYU HY-1500 can load jumbo rolls up to 1500 mm in diameter with pneumatics, which makes the job easier for the user and cuts down on switching time.
- Embossing unit: Steel-to-steel edge embossing keeps plies from separating and adds a unique tactile feel. Single and double embossing patterns cater to different price points in retail, such as value, mid-range, and premium. Manufacturers can change their products to fit store planograms without having to retool because the platform has three different embossing setups.
- Rewinding and perforating: Four high-precision screw knives make perforations that are accurate to within ±3 mm. Customizable perforation pitch (85–135 mm or 170–260 mm) meets sheet-count norms in foreign, Middle Eastern, and North African markets.
- Core feeding and coreless winding: Cores with standard sizes of 30–60 mm can be fed automatically by core feeding. An extra coreless module lets you make eco-friendly rolls, which is becoming more important as rules to cut down on plastic get stricter in the GCC and EU.
- Glue spraying, tail sealing, and edge trimming: All three tasks are automatic and controlled by a PLC that keep the finish clean without any help from an operator.
It's like one environment here at these stations. The PLC + Touch Screen (HMI) management design connects them, letting you see the diameter in real time, stopping the machine instantly when a sheet of paper breaks, and getting the same output over long runs. At scale, the amount of automation means a lot. A full-servo line moving at 180–240 m/min can handle a lot more parent roll material per shift than a semi-automatic line, and it can also keep the measurements more accurately, which is necessary for private-label supply contracts with supermarkets.
How Toilet Paper Manufacturing Equipment Works: From Raw Material to Finished Product
Workflow From Parent Roll to Consumer-Ready Tissue
The process starts with getting the parent rolls ready. The unwind stand is run through toilet paper manufacturing equipment jumbo rolls, which are usually 13–30 gsm and one or two ply. The rolls are filled pneumatically. Web tension control at this stage stops tiny tears that would otherwise cause paper to break further down the line. After that, the web goes through the embossing nip. The depth and pattern of the emboss are set based on the product specifications.
The continuous web goes into the rewinding area after being embossed. It is wound onto a cored or coreless mandrel with a controlled width. The HY-1500 can handle finished roll diameters of 90 mm to 150 mm, which is the full range of forms for market bathroom tissue. The web is scored by perforation blades at set times. Checking the blades every 8–12 hours of use and replacing them every 15–30 days, based on how rough the paper is, keeps the separation of sheets clean and reduces customer complaints.
When a log reaches the desired diameter, tail sealing glue is automatically applied, and the log is moved to the bandsaw cutter to be cut into rolls that are the right length for stores. Trimming the edges gets rid of selvage waste. After the rolls are ready, they are packed up. Practical maintenance discipline underpins uptime. Vibration analysis at rated speed finds misaligned shafts before they cause unplanned downtime. Before the toilet paper manufacturing equipment is shipped, it goes through factory acceptance testing (FAT) on the client's own GSM standard. This is usually a steady four-hour run that makes sure the emboss level and glue coverage stay the same.
Comparing Tissue Converting Machines: Making the Right Investment Decision
Evaluating Capacity, Flexibility, and Total Cost of Ownership
In the end, choosing a machine comes down to balancing three factors: the estimated production speed, the freedom of the product configuration, and the total cost of ownership over the next five to seven years. Basic semi-automatic rewinders can handle narrower parent rolls at slower speeds and are good for small and medium-sized converters that are just starting out and don't have a lot of money to spend on equipment. Full-automatic lines like the HY-1500, which can work at speeds of 180–240 m/min and have a working width of 1500 mm, meet the needs of makers who serve current retail chains in terms of throughput and audit readiness.
According to RISI/Fisher International tissue market data, as yearly output rises, high-speed converting lines regularly offer lower per-unit converting costs. OEMs from Europe, like Fabio Perini and Toscotec, are known for making high-end products with precise engineering. The HY-1500 from HENGYU is a unique value because it is CE-certified, ISO-aligned, and has been used in over 20 countries. It also comes with a one-year quality guarantee and 24/7 after-sales support, all of which are important factors for procurement teams going through audits of toilet paper manufacturing equipment. The power to be coreless deserves its own discussion. The global coreless tissue market is growing as stores respond to sustainability and packaging reduction laws. A machine that switches between cored and coreless modes without a full retool protects product portfolio flexibility.
Procurement Strategies for Tissue Converting Equipment
Supplier Evaluation Criteria That Protect Capital Investment
There's more to choosing a tissue machinery supplier than just looking at the specs on a datasheet. These are the things that skilled toilet paper manufacturing equipment procurement teams look for:
- Verified CE and ISO certification: The CE mark shows that the product meets the safety standards of the EU Machinery Directive. ISO 9001 makes sure that the consistency of the manufacturing process is checked by a third party. Both must be met by producers who serve supermarket groups and are subject to factory checks.
- After-sales SLA and spare parts availability: A promise of technical support 24 hours a day, seven days a week, with documented response times keeps production going. Video guidance and remote troubleshooting are both part of HENGYU's lifetime technical support program. Over 95% of setups are ready for production with just remote guidance.
- Factory acceptance testing protocol: Reliable providers test your specific grade of paper with FAT before sending it to you. This method, which is explained in ISO 9001 supplier qualification literature, is the most reliable quality check that buyers can do before the goods are delivered.
- Export experience and logistics coverage: The EXW, FOB, CIF, and door-to-door choices make it easier for buyers to manage payment processes and port-of-entry clearance for letters of credit.
Before signing the contract, the custom design, such as the range of roll diameters, hole pitch, and emboss pattern, should be confirmed in writing. Buying used equipment is cheaper, but it usually doesn't come with a guarantee and may need to be fixed up to meet current safety standards.
Future Trends and Technological Innovations in Tissue Machinery
IoT-enabled condition monitoring is being used in the tissue converting industry. Sensors send data about vibration, temperature, and tension to dashboards that look for problems before they happen. AI-assisted quality vision systems check the stamp depth and accuracy of the perforations at line speed, instead of sampling by hand.
The use of energy is another area of active development for toilet paper manufacturing equipment. Variable Frequency Drives (VFDs) lower the amount of energy that motors need to run during cycles of speeding up and slowing down. This can help with facility energy audits. Coreless production gets rid of the need for and weight of core materials, which lowers the cost of raw materials and the carbon footprint of shipping. These are all good things for manufacturers who are responding to retailers' ESG scorecards. Planning for scalability should start with choosing the right tools. A machine platform that can accept modular upgrades—such as online slitting, more embossing units, and automated packing integration—makes assets last longer and delays the need to buy new ones.
Conclusion
The success of tissue conversion rests on how well the machine's capabilities are matched to the needs of the market. The right production line lowers the cost per unit, lets you differentiate your products with emboss and coreless choices, and can handle the close scrutiny of audits that modern retail outlets demand. The HY-1500 from HENGYU meets these needs with its 180–240 m/min operating range, three embossing configurations, dual core/coreless capability, and full PLC control. The toilet paper manufacturing equipment comes with CE approval and lifetime technical support from a provider with more than 20 years of experience in the field.

FAQ
What production speed should I target for a supermarket supply contract?
Most modern retail buyers expect converting lines to go at least 180 m/min so they can meet their volume obligations. The HY-1500 works at speeds of 180 to 240 m/min, which is fast enough for normal industrial tissue volumes and has room for growth in demand.
How often do perforation blades require servicing?
Every 8–12 hours of use, the condition of the blades should be checked. Depending on the GSM standard and how rough the paper is, the gaps between sharpening or replacing them are usually between 15 and 30 days.
Can one machine produce both cored and coreless rolls?
Yes. These days, rewinding platforms can work in two different modes. The HY-1500 has an extra coreless module that can be used to switch between mandrel-based winding and coreless winding without having to retool the toilet paper manufacturing equipment completely.
What certifications matter most for factory audits?
CE marking and ISO 9001 certification are the basic requirements that most supermarkets and other large buyers look for when they are qualifying suppliers.
What footprint does a full-automatic line require?
A standard fully automatic converting line with a rewinder, a log saw, and packaging needs at least 20 m × 8 m of floor space.
Ready to Scale Your Tissue Production? Contact HENGYU Today
Engineers from HENGYU can look over your production goals, building layout, and desired product specs. With a known global track record as a provider of toilet paper manufacturing equipment, we can make sure that every HY-1500 setup meets your exact converting needs, from the number of holes to the design of the embossing and the ability to work without a core. Reach our technical team directly at doris@hytissuemachine.com or visit hytissuemachine.com to request a detailed quotation and equipment proposal.
References
1. TAPPI — Tissue Converting Operations and Blade Maintenance Guidelines, TAPPI Journal, 2022.
2. Fisher International — Global Tissue Market Outlook: Cost Benchmarking for Converting Operations, 2023.
3. European Commission — Machinery Directive 2006/42/EC: CE Marking Requirements for Industrial Equipment, 2023.
4. PITA (Paper Industry Technical Association) — Smart Manufacturing and IoT Integration in Tissue Production, Paper Technology International, 2023.
5. U.S. Department of Energy — Variable Frequency Drives: Energy Savings in Industrial Motor Systems, Energy Efficiency & Renewable Energy, 2022.
6. ISO — ISO 9001:2015 Quality Management Systems — Requirements, International Organization for Standardization, 2015.